Severe Service Valves
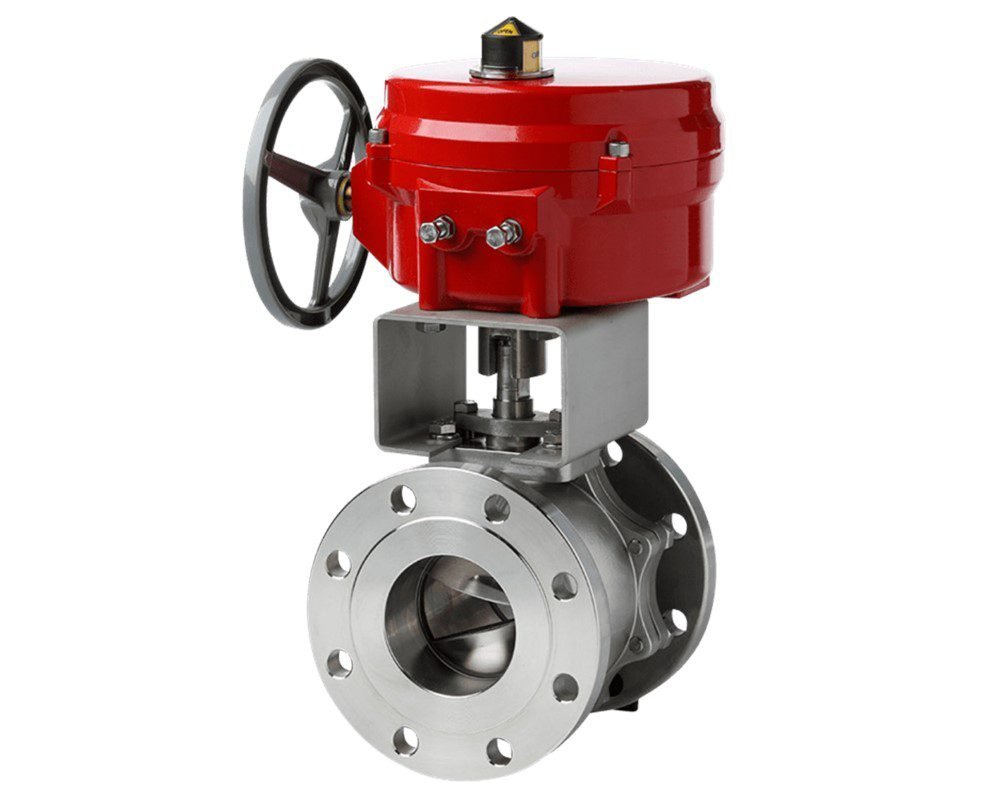
Severe Service Slurry Ball Valve
Metal-seated ball valve with hard coatings for abrasive slurries in mining and minerals processing.
Overview
In harsh environments where pipelines transport abrasive or corrosive slurries, severe service slurry ball valves play a vital role. These valves are specifically designed to withstand the demanding conditions of these applications, ensuring reliable flow control and minimizing downtime.
Key features
- Carbon Steels, Low Temperature Carbon Steel, Martensitic Steels, Austenitic Stainless Steel, Duplex Stainless Steels, Super Duplex Stainless Steels, Nickel Alloys, Nickel Aluminum Bronze, Hastelloy, Inconel, Titanium Alloy & Carbon Steel with Internal Corrosion Resistant Alloy (CRA) Overlay
- Carbon Steels, Low Temperature Carbon Steel, Martensitic Steels, Austenitic Stainless Steel, Duplex Stainless Steels, Super Duplex Stainless Steels, Nickel Alloys, Nickel Aluminum Bronze, Hastelloy, Inconel, Titanium Alloy & Carbon Steel with Internal Corrosion Resistant Alloy (CRA) Overlay
- Heavy-Duty Construction: Constructed from robust materials like high-chromium alloy steels or abrasion-resistant castings to endure the wear and tear caused by slurries.
- Metal Seating: Employ metal seats (e.g., tungsten carbide, Stellite) instead of softer materials like PTFE (Teflon) to provide superior wear resistance against abrasive particles in the slurry.
- Anti-Clog Design: The internal design minimizes areas where slurry can accumulate and solidify, reducing the risk of blockages and ensuring smooth flow. This may include features like streamlined flow paths or flushing ports.
- Blow-Out Proof Stem: The stem design prevents the wellhead (the top portion of the valve assembly) from separating from the body in case of high pressure, ensuring safety and operational integrity.
- Bidirectional Flow Capability (Optional): Some severe service slurry ball valves can handle flow in either direction, offering operational flexibility.
- Forged compact body with precision machined construction complies to ASME B16.34.
- The optimized body includes several features for easy installation in various orientations.
- Wall thickness is larger than required by industry standards and ideal for corrosion and erosion applications.
- Robust blowout-proof fully guided stem, has the largest Maximum Allowable Stem Torque (MAST) of all severe service ball valves, ensuring normal operation regardless of valve orientation and process conditions.
- External thrust bearing is positioned away from corrosive media, reducing the operating torque and extending valve performance.
- Ball and seats are 100% fully mate-lapped and coated with the latest coating solutions that fit the requirements of the service conditions.
- Advanced coatings for ball and seats, as well as the waterway bore when necessary, provide trouble free operation even in aggressive erosive and corrosive services as demonstrated in the most severe HPAL plant in the world. Several deposition methods are available and some of these processes provide greatly improved wear properties.
- Our stem packing technology guarantees a low-emission stem seal in compliance with the highest industry standards.
- Slurry-proof floating upstream seat with unique precision machined ‘load ring’ guarantees permanent contact between the ball and seats for effective ball scrapping and tight shut-off in both directions.
- Seats are replaceable in-line for simple assembly and disassembly, with no special tools required.
- A variety of body and trim material options are available offering extra corrosion allowance.
Technical specifications
- Size Range
- 1/2 – 16 NPS, DN15 - DN400
- Body Materials
- Temperature Range
- -29°C to 450°C
- Trim Materials
- Maximum Allowable Operating Pressure
- ASME 150# to 900#
- Pressure-Temprature Rating
- ASME B 16.34
- Construction Details
- Bolted Bonnet
- Body Style
- Flanged End, Butt Weld
- Design Standard
- ASME B16.34
- Flange Drilling
- ASME B16.5
- Testing Standard
- API 598, ISO 5208, BS 6364
- Face To Face
- ASME B16.10
- Applications
- Refineries,Hydrocarbon,Energy and Process industries.
- Operation
- Handwheel, Gear, Actuator (Pneumatic, Hydraulic, Electro-Hydraulic and Electric Motorised)
Applications
- Refineries
- Hydrocarbon
- Energy and Process industries.
Benefits
- Extended Service Life: Durable construction and wear-resistant materials ensure the valve can function reliably for extended periods in harsh slurry environments.
- Reduced Maintenance: The anti-clog design and robust materials minimize maintenance requirements compared to valves susceptible to clogging or wear.
- Reliable Shutoff: Metal seating provides a secure seal even with abrasive slurries, preventing leakage and ensuring proper flow control.
- Improved Safety: Blow-out proof stem design enhances safety by preventing catastrophic failures under high pressure.
- Versatility (Optional): Bidirectional flow capability allows for more flexible piping configurations.
Frequently asked questions
- **Slurry properties:** Consider the abrasiveness, corrosiveness, and particle size of the slurry.
- **Pipe size and flow rate requirements:** Choose a valve with the appropriate size and flow capacity.
B. What are the advantages of metal seating compared to soft seating materials?
- Provides a more reliable seal over a longer service life.
- Severe service valves are specifically designed with robust materials, anti-clog features, and blowout-proof stems to withstand the demanding conditions of slurry applications. Standard ball valves may not be suitable for these harsh environments.
Regular inspection is recommended to monitor wear, ensure proper operation, and identify potential issues. The specific maintenance schedule will depend on the operating conditions, valve design, and manufacturer’s recommendations.
[Download](https://nishthaglobal.com/severe-service/severe-service-slurry-ball-valve/#)
Application engineering
Specify your requirement.
Share your process conditions, required configuration and quantity. Our team will confirm suitable options and available documentation.
Thank you — enquiry received
An application engineer will review your requirement and reply within one working day.